An intermittently bonded ribbon production system is used to manufacture flexible fiber groups for contemporary, high-count cable architectures. It keeps fibers properly aligned for expedited mass fusion splicing, yet allows the fiber group to remain flexible within a compact cable core.
Compared with continuously bonded ribbons, intermittent bonded ribbons feature discrete bonding points at predetermined intervals. This strategic placement enables the fibers to maintain alignment while the ribbon can flexibly roll into circular loose tubes and other confined spaces.
Network engineers employ this method when faced with constraints in duct space, splice closures, and equipment racks. A meticulously crafted ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.
Fiber Coloring Machine
Fiber Coloring Machine
Fiber Secondary Coating Line
Important Points
- A bonded ribbon production system supports compact and flexible fiber layouts.
- Localized bonds keep optical fibers aligned while preserving ribbon flexibility.
- Flexible ribbons support higher fiber counts within small circular cable constructions.
- Mass fusion splicing is faster when fiber order remains stable and clear.
- Ribbon cable systems support data centers, telecom backbones, and fiber access networks.
Overview Of An Intermittent Bonded Ribbon Production Line
This ribbon production method enables the creation of fiber designs that harmonize density with practicality. This method involves placing bonds at predetermined intervals, allowing for the movement of fiber subunits between these points.
This technique facilitates the incorporation of a higher number of fibers within constrained duct spaces. It also ensures the preservation of the organized ribbon structure, essential for efficient splicing and cable assembly processes.
How Does An Intermittently Bonded Optical Fiber Ribbon Work?
A flexible intermittently bonded optical ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds remain relatively free, enabling the ribbon to adopt various configurations without rigidification.
This ribbon format is commonly described as a rollable, flexible, or spider web ribbon. It contrasts with the conventional flat ribbon cable, which maintains a fixed profile along its entire length.
For splice preparation, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers create space-efficient bundles, optimizing space utilization within the cable.
Why High-Density Networks Use Flexible Ribbon Technology
Fiber network planners must address the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure helps ribbon groups pack into smaller cable cores, preserving fiber order.
The fiber density ratio is a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding can improve this ratio, allowing ribbon groups to occupy available spaces within the cable.
For network installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.
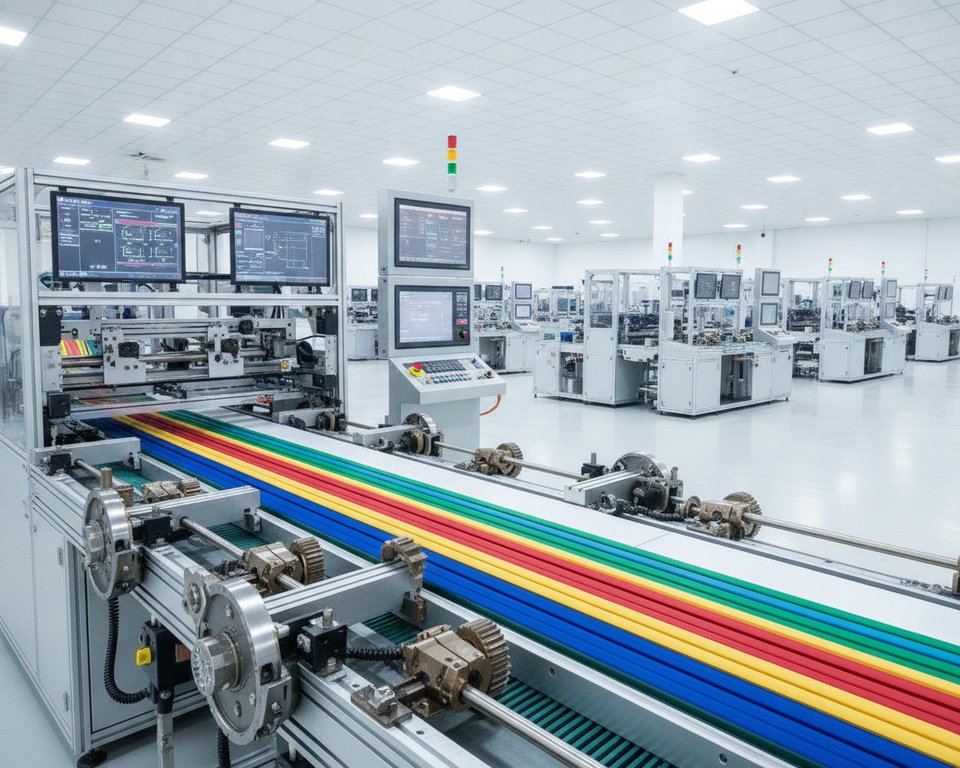 Intermittent Bonded Ribbon Production Line
| Ribbon Feature | Intermittently Bonded Design | Continuously Bonded Ribbon |
|---|---|---|
| Bonding pattern | Individual bond points at controlled spacing | Continuous bonds along the ribbon length |
| Fiber shape between bonds | Can bend, roll, or fold for dense packing | Maintains a largely fixed flat profile |
| Splicing configuration | Can be flattened for mass fusion splicing | Remains permanently in a flat ribbon configuration |
| Role in cable packing | Enables dense placement of flexible fiber subunits | Relies on a relatively rigid ribbon stack |
| Typical cable application | Flexible ribbon and high-density fiber cable designs | Conventional fixed ribbon cable structures |
Construction And Material Requirements For Intermittent Bonded Ribbon
An intermittent bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture supports compact cable arrangements while allowing effortless separation during handling, routing, and splicing.
Choosing appropriate materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must maintain its fibers securely without imparting undue stiffness to the ribbon.
Fiber Count And Subunit Arrangement
Intermittent bonded ribbons can accommodate 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.
A 12-fiber configuration often employs six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.
Controlled gaps introduced between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.
| Construction Element | Typical Configuration | Process Purpose |
|---|---|---|
| Ribbon fiber count | 4, 8, 12, 24, or as many as 36 fibers | Supports required cable density and fusion splice capacity |
| Subunit layout | Pairs of adjacent fibers within each subunit | Supports controlled separation between groups |
| Fiber spacing in a subunit | Contacting fibers or spacing of no more than 1.5 fiber diameters | Keeps the subunit profile compact and stable |
| Spacing between subunits | A typical range of 5 to 100 micrometers | Allows greater movement and flexibility near bond points |
UV-Curable Resin And Wet-On-Wet Bonding
The subunit coating and bond material frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.
Wet-on-wet bonding produces a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.
UV-curable resin materials can blend at the interface before curing. This supports molecular interaction between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.
Core Equipment In An Intermittent Bonded Ribbon Production Line
A fiber ribbon line integrates advanced motion control with meticulous material handling. Each station maintains fiber cleanliness, alignment, and stability from the initial payoff to the final winding.
The equipment facilitates adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to craft a flexible custom ribbon cable, preserving the integrity of the fiber order.
Fiber Payoff With Tension Control
Fiber payoff systems feed individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.
Within a fiber ribbon production line, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.
Coating Die And Discrete Bond Applicator
A coating die places a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.
A discrete bond applicator then places a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.
| Equipment | Primary Function | Process Benefit |
|---|---|---|
| Payoff tension system | Supplies fibers under controlled tension | Minimizes twisting and uneven fiber loading |
| Fiber coating die | Forms coated fiber subunits | Keeps subunit dimensions and shape consistent |
| Intermittent bond applicator | Deposits resin at set intervals | Creates flexible links between adjacent subunits |
| UV curing and take-up unit | Cures, cools, inspects, and winds the ribbon | Protects bond quality and preserves fiber order |
UV Curing, Cooling, And Ribbon Winding Equipment
UV lamps cure the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.
Cooling equipment lowers ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.
Take-up equipment winds the finished ribbon with low, even tension. Proper winding preserves the finished bonded structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.
Fiber Alignment, Preparation, And Color Sequence Management
Reliable ribbon cable production starts with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.
Managing Fiber Identification During Splicing And Maintenance
A clearly defined fiber color sequence is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.
For higher fiber counts, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.
| Fiber Number | Fiber Identification Color | Process Purpose |
|---|---|---|
| 01 | Blue | Starts the standard fiber color sequence |
| 2 | Standard orange | Allows quick identification during handling |
| 03 | Green | Helps preserve the established fiber order |
| 04 | Brown | Helps verify subunit placement |
| 05 | Standard slate | Creates a clear mid-sequence identifier |
| 6 | White | Supports clear visibility during inspection |
| 07 | Standard red | Improves traceability in splicing records |
| 08 | Black | Helps technicians recognize sequence position in trays |
| 09 | Yellow | Assists field restoration activities |
| 10 | Violet | Separates late-sequence fibers clearly |
| 11 | Standard rose | Supports high-count ribbon identification |
| 12 | Standard aqua | Marks the final position in the standard color order |
Avoiding Fiber Twist And Tension Imbalance
Payoff units and guides are instrumental in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.
Production personnel carefully check tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.
Intermittent Bond Application With UV Curing
Intermittent bonding integrates fiber subunits without solidifying the ribbon into a rigid form. This method supports compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.
Applying Intermittent Bonds At Predetermined Intervals
Bond applicators place resin at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.
A controlled applicator deposits a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends reduce sudden stress transitions when the cable bends or twists.
Creating Strong, Flexible Bond Interfaces
Wet-on-wet processing requires applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.
The resulting material gradient affects various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features help the bond resist peeling while facilitating separation when required.
Controlling UV Curing Performance
The UV lamps must supply consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.
Operators closely monitor bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.
Flexible Flat Cable And Fiber Ribbon Quality Control
Ensuring each flat ribbon cable’s integrity is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.
Regular inspections are critical in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.
Bond Spacing, Ribbon Width, And Thickness Inspection
The spacing between bonds is a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.
Inspection protocols are in place to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.
| Inspection Point | What Is Checked | Quality Benefit |
|---|---|---|
| Fiber identity | Count, identification color, and fiber position | Supports reliable splice records and maintenance activities |
| Bonding pattern | Bond placement, separation distance, and subunit joining | Maintains flexibility and fiber organization |
| Ribbon geometry | Width, thickness, and flatness | Ensures the ribbon works with downstream handling and splicing tools |
| Ribbon surface condition | Cure quality, coating completeness, and visible defects | Helps minimize handling damage during winding |
Mechanical And Optical Performance Testing
Mechanical evaluations examine on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.
Optical testing encompasses evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.
Attenuation checks and splice-related handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.
Precision Winding, Automation, And Production Efficiency
The essence of efficient ribbon production on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.
Production Line Synchronization And Process Data Monitoring
Production controls coordinate payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.
Manufacturing data records capture fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.
- Controlled payoff tension reduces fiber stretching and slack.
- Bond timing ensures consistent intervals between discrete joints.
- Regular dimensional checks reveal ribbon width or thickness deviations early.
- Take-up data helps with production lot tracking and later processing.
Preparing Wound Ribbon For Downstream Cable Manufacturing
Precision winding equipment ensures the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.
Completed ribbon packages can be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.
For customized ribbon products, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.
| Monitoring Area | Primary Control Focus | Downstream Benefit |
|---|---|---|
| Payoff section | Stable tension and correct color sequence | Consistent ribbon organization during cable assembly |
| Bond application | Consistent spacing and resin volume | Flexible ribbon behavior during handling |
| UV cure stage | Controlled lamp output and exposure time | Consistent bond strength prior to take-up |
| Precision ribbon winder | Even traverse, spool tension, and layer control | Smooth payout for central tube or loose tube loading |
Applications, Splicing, And Connector Planning For Ribbon Cable
Ribbon fiber is widely used in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.
A carefully designed ribbon cable assembly enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.
Benefits Of Mass Fusion Splicing
A ribbon fusion splicer allows the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.
This approach minimizes handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.
In contrast, loose tube cable necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.
Planning Connections For Dense Fiber Links
High-density fiber links often employ MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.
System planning must also account for transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.
| Planning Item | What It Controls | Common Application |
|---|---|---|
| Number of ribbon fibers | Required splice capacity and cassette configuration | 12-fiber and 24-fiber network backbones |
| MPO/MTP cable connector | Polarity management and equipment port compatibility | Data center trunks and 5G equipment rooms |
| Multi-fiber harness or fanout assembly | Transition from multi-fiber connections to single-fiber ports | Switch connections and patching fields |
| Optical link loss budget | Maximum allowable loss through connectors, splices, and cable length | High-speed optical transmission routes |
Shanghai Weiye OFC Equipment For Ribbon Line Projects
Shanghai Weiye OFC Equipment, also known as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to ensure consistent processing, facilitate clear operator control, and enable seamless integration into production lines.
For initiatives requiring an intermittent bonded ribbon production line, SHWY supports every stage of ribbon handling, curing, and winding with suitable machinery.
SHWY Experience In Optical Fiber And Cable Machinery
Established in 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.
SHWY became independent in 2020, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.
Relevant Production Equipment From SHWY
SHWY offers a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.
For ribbon projects, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.
The broader SHWY portfolio also includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.
Final Thoughts
An intermittent bonded ribbon production line integrates fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step maintains organized fiber positioning while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.
The resultant ribbon cable supports efficient mass fusion splicing and organized fiber management. It is well suited to applications involving high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.
Comprehensive project planning reaches beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.